Manufacturing Data Integration: Why It Matters on the Factory Floor
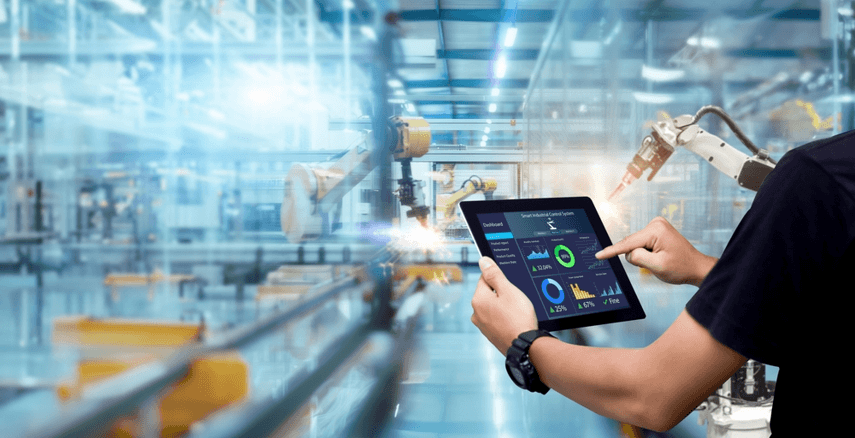
A typical factory produces a steady stream of data throughout the day. Output figures come from the line, downtime gets recorded, inspections create another set of records, and maintenance has its own history. The information is there. Finding the piece you need at the moment you need it is often the harder part.
A production manager, for example, may be focused on whether a line is keeping pace with the day’s target. Maintenance is looking at equipment behavior and repair history. Quality has inspection results to review, while ERP systems hold orders, inventory, and scheduling information. Suppliers add another layer with records covering materials, components, and deliveries.
In many plants, these systems were introduced at different times and for different reasons. Some machines send data automatically. Others still depend on an operator entering information by hand. Quality may use one platform while maintenance uses another.
That setup can work perfectly well until a problem crosses more than one of those systems.
This is where manufacturing software and data integration can be useful. Instead of searching several places to understand a production event, teams can bring the relevant information together and see more of the story in one place.
What Does Manufacturing Data Integration Mean?
Manufacturing data integration is essentially about getting separate systems to exchange useful information.
There is no single setup that every plant needs. One manufacturer may want machine data connected to its ERP. Another may need inspection results alongside production records. A plant dealing with frequent equipment stops might get more immediate value from linking machine activity with maintenance history.
Depending on the operation, this could involve PLCs, sensors, SCADA, ERP software, MES platforms, maintenance applications, warehouse systems, scanners, and quality tools.
The aim is not to connect everything simply because the technology allows it. The useful connections are the ones that help people answer questions they regularly face on the factory floor.
Why Factory Data Ends Up in Different Places
Manufacturing technology tends to grow piece by piece.
An ERP may have been installed years before a newer production line arrived. Maintenance might later adopt its own application. Quality could still rely partly on spreadsheets. Even machines working a few feet apart may record and communicate data differently.
Usually, the gaps become obvious when something unexpected happens.
Consider a sudden increase in scrap. Inspection records can show which products failed, but they may not explain what changed. To get closer to an answer, the team might compare the affected units with the materials being used, equipment settings, recent service activity, line speed, and the shift during which they were produced.
If those details live in separate systems, the investigation starts with gathering records rather than investigating the actual problem.
Connecting the Production Plan with Reality
Production schedules describe what should happen. Conditions on the floor determine what actually happens.
Take a daily order for 5,000 units. The morning starts normally, but a changeover runs longer than planned. Later, several short equipment stops cost the line more production time. By midday, the original target has not changed, yet the line is already running behind it.
If current shop-floor information reaches the planning system, that gap becomes visible while there is still time to respond.
Planners can see the delay developing during the shift rather than learning about it after production closes for the day. Depending on the situation, they can then review the remaining schedule, available people, other orders, or capacity elsewhere in the plant.
Quality Investigations Become Easier
A failed inspection tells the quality team there is a problem. It rarely tells them the whole reason behind it.
Were all the rejected units produced on one machine? Did they share a material batch? Was a setting changed before the run? Had work recently been carried out on the equipment?
Those questions often require records owned by different departments.
With disconnected systems, somebody has to collect the information before meaningful analysis can begin. When relevant records are linked, the team can spend less time assembling the history and more time examining what changed.
Integration will not automatically identify the root cause. What it can do is put more of the evidence in one place.
Maintenance Gets More Context
A service log is useful for seeing when a machine was repaired or inspected, but it does not always show what was happening between those events.
The production history can fill in some of those blanks.
Perhaps a line is still operating, but each cycle is taking a little longer than it did last month. Short interruptions that once happened occasionally may now be showing up several times during a shift. An alarm may also be appearing more often than it used to.
On their own, these observations may not mean much. Alongside previous service records and machine history, however, they give maintenance technicians more context when they begin looking into an equipment issue.
Less Time Spent Copying Information
Some integration problems are far less technical.
In plenty of plants, the same number still gets handled several times. An operator records production output, a supervisor adds it to a spreadsheet, and later another employee enters the figure into an ERP or reporting tool.
The process works, but it creates extra steps and more opportunities for mistakes.
Where systems can exchange the information directly, much of that repetitive entry can be reduced. People remain important because a production number rarely explains everything that happened during a shift. Their time, however, can be spent adding that explanation rather than typing the same figure into several places.
What About AI in Manufacturing?
Predictive maintenance, automated quality analysis, anomaly detection, forecasting, and production optimization are attracting plenty of attention. Before any of those applications can do much useful work, there is a less glamorous question to answer: is the underlying factory data in good shape?
A sophisticated model will not make inconsistent records consistent. It also cannot recover information that was never collected in the first place.
This is why the work done before an AI project can matter as much as the model itself. Manufacturers need to understand where their production data comes from, how reliable it is, and whether records from different systems can be connected in a meaningful way.
Getting those basics in order gives analytics and AI projects something much stronger to build on.
Security Still Matters
Connecting previously separate systems changes how information moves around a plant, so security needs to be part of the discussion from the beginning.
A useful starting point is knowing exactly what is connected to what. From there, teams can determine which employees or external parties require access and what level of access is appropriate.
Network boundaries, user permissions, authentication methods, API access, recovery procedures, and connections used by outside partners all deserve attention.
More connected operations can be useful, but every connection should have a reason to exist. If a system does not need access to certain production information, there is little value in giving it that access.
Start with a Problem Worth Solving
Trying to integrate an entire plant in one project can quickly become complicated. A smaller starting point is often easier to manage.
Look at a question that repeatedly sends people searching for answers.
Why did a particular line lose two hours yesterday? What changed before scrap began increasing? Why does the ERP show material in stock when the production team cannot locate it? What is behind the recurring stops on one machine?
Pick one of those questions and trace the information needed to answer it.
That exercise usually reveals which systems need to communicate first. It also gives the integration project a practical purpose that people on the floor can understand.
Conclusion
A factory does not necessarily need more data. It may simply need a better way to use the information already being produced.
One part of an incident might sit with production, another with maintenance, and another inside a quality or inventory system. When those pieces can be viewed together, the picture becomes easier to understand.
For people doing the day-to-day work, the benefit is fairly practical. There is less time spent collecting reports, more context when something goes wrong, and a better chance of spotting production issues while there is still time to act.
That same groundwork can later support analytics, automation, and AI.
Ultimately, manufacturing data integration should solve an everyday problem: when a team needs to find out what happened on the floor, getting the answer should not turn into a search through several applications, spreadsheets, and departmental records.
